










Anuh Pharma lifts Tarapur API capacity to 2,975 MTPA
Key highlights
- Anuh Pharma inaugurated its 575-MTPA Tarapur Unit F-10 on 20 October 2026.
- F-10 takes Anuh Pharma’s stated total API capacity to 2,975 MTPA.
- The new site has two API blocks, one intermediate block and approximately 69 KL of reactor capacity.
- F-10 occupies approximately 9,500 square metres and includes quality-control and finished-goods warehouse capacity.
powered by IRIS
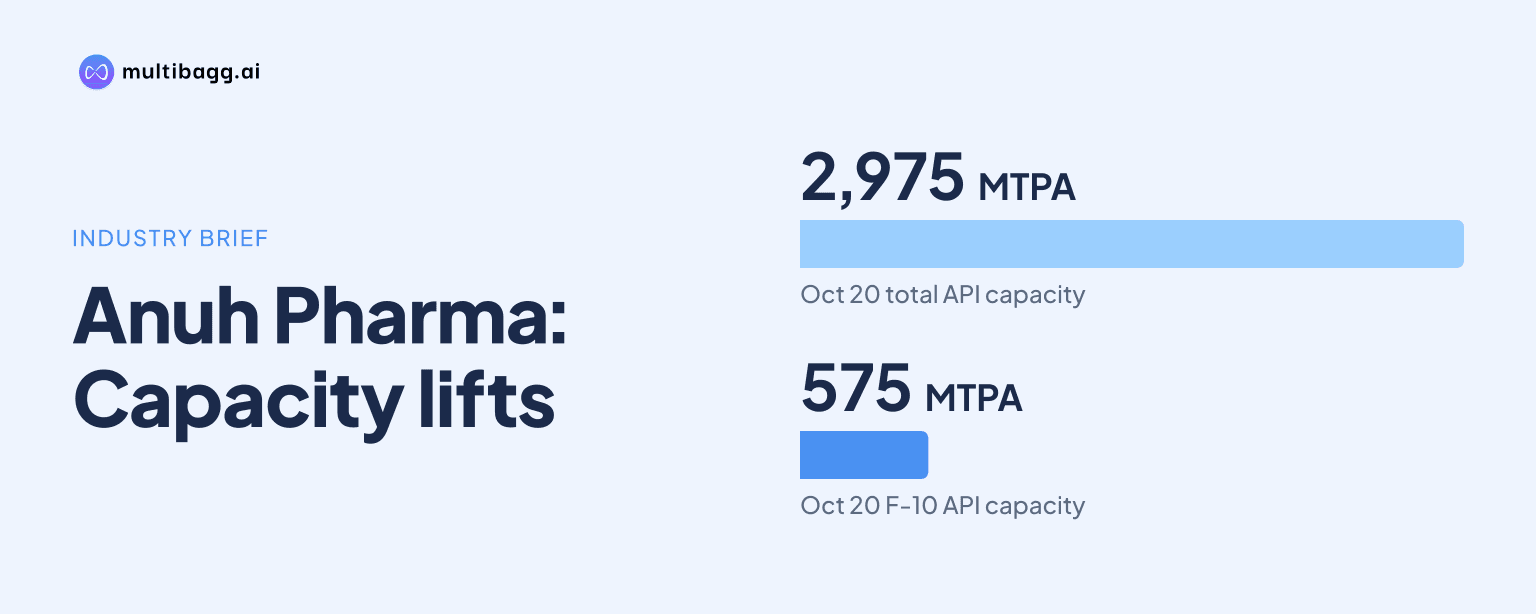
Anuh Pharma Ltd. commissioned Tarapur Unit F-10 on 20 October 2026, adding 575 metric tonnes per annum (MTPA) of active pharmaceutical ingredient (API) capacity and taking its stated total API capacity to 2,975 MTPA. The new unit includes two API blocks, one intermediate block, in-house quality-control facilities and a finished-goods warehouse.
Know Anuh Pharma inside out
Results, valuation, peers and who's buying, in one view.
What does the F-10 commissioning add to Anuh Pharma?
F-10 adds 575 MTPA of installed API capacity through a multi-purpose current Good Manufacturing Practice (cGMP) facility in the MIDC Tarapur industrial area at Boisar. Anuh Pharma describes the multi-storey plant as designed for multi-purpose API manufacturing and located in the same industrial area as its Tarapur E-17 and E-18 units.
The unit combines production, quality control and warehousing infrastructure at an approximately 9,500-square-metre site. It has two API blocks and one intermediate block, while a dedicated finished-goods warehouse provides storage capacity for manufactured products.
F-10 has approximately 69 kilolitres (KL) of total reactor capacity, including stainless-steel and glass-lined reactors of up to 6.3 KL. Its listed production equipment includes centrifuges, agitated nutsche filter dryers (ANFD), fluid-bed dryers, rotocone dryers and tray dryers.
How does F-10 change Anuh Pharma’s API capacity?
F-10 takes Anuh Pharma’s stated total API capacity to 2,975 MTPA, including the 575-MTPA expansion. Based on the stated total capacity and the F-10 addition, pre-expansion capacity was implied at 2,400 MTPA, making the addition equivalent to 575 MTPA.
Anuh Pharma states that its Tarapur manufacturing facility has 11 API blocks and three intermediate blocks within the 2,975-MTPA capacity total. F-10 contributes two API blocks and one intermediate block, making it an expansion of both production capacity and the company’s disclosed manufacturing-block infrastructure.
The broader Tarapur manufacturing facility covers 20,920 square metres and is described by Anuh Pharma as a United States Food and Drug Administration (US FDA), European Union Good Manufacturing Practice (EU GMP) and World Health Organization (WHO) pre-qualified site. The company specifically states that the 2,975-MTPA total includes the new capacity.
What quality systems does Anuh Pharma F-10 have?
F-10 has in-house quality-control and microbiology facilities, including high-performance liquid chromatography (HPLC), gas chromatography (GC), gas chromatography-headspace (GC-HS), total organic carbon (TOC) testing, Fourier-transform infrared spectroscopy (FTIR) and stability chambers. Anuh Pharma says these systems are server-connected.
The plant has purified-water capability meeting Indian Pharmacopoeia (IP), British Pharmacopoeia (BP), European Pharmacopoeia (EP) and United States Pharmacopeia (USP) requirements. Anuh Pharma also says F-10 is being integrated into its group-wide quality-management system.
The F-10 facility includes zero-liquid-discharge effluent treatment based on an effluent-treatment plant (ETP) and reverse osmosis (RO), along with advanced solvent recovery. At the wider Tarapur facility, Anuh Pharma says its zero-liquid-discharge system treats 100% of generated pollution.
Got a follow-up? Ask IRIS
What infrastructure supports the Tarapur manufacturing network?
Anuh Pharma’s Tarapur network combines the new F-10 site with existing E-17 and E-18 units in the MIDC Tarapur industrial area at Boisar. F-10 adds an approximately 9,500-square-metre multi-storey production block, while the company separately reports a 20,920-square-metre manufacturing facility with 11 API blocks and three intermediate blocks.
The new unit provides dedicated production, quality-control and finished-goods warehousing functions, while the broader Tarapur facility has supporting infrastructure including a green belt, fire-fighting and safety measures, an adjoining office and a staff training hall. Anuh Pharma also reports 100% power backup through a dedicated line from the power distributor.
F-10’s approximately 69-KL reactor capacity supports its stated multi-purpose manufacturing role, rather than a product-specific line identified in the presentation. The company does not disclose which API products will be made at F-10, capacity utilisation, or a timetable for commercial output from the 575-MTPA facility.
How is F-10 positioned within Anuh Pharma’s operations?
F-10 is positioned as a multi-purpose API facility with production, testing, effluent treatment and warehousing functions at one site. Its two API blocks and one intermediate block sit within Anuh Pharma’s stated 2,975-MTPA manufacturing capacity, which includes the new expansion.
Anuh Pharma identifies Vivek B. Shah, Joint Managing Director, as responsible for manufacturing operations and research and development since 2009. The presentation also identifies a general manager for quality with more than 27 years of pharmaceutical quality-management experience and a general manager for research and development with 25 years of industrial process-research experience.
The expansion’s operational framework includes in-house testing instruments, purified-water systems and zero-liquid-discharge treatment. These features support the company’s stated plan to integrate F-10 into the group-wide quality-management system, but the presentation does not provide production-volume or revenue targets for the unit.
Conclusion
F-10 increases Anuh Pharma’s disclosed API capacity by 575 MTPA to 2,975 MTPA and adds two API blocks, one intermediate block and approximately 69 KL of reactor capacity. The Tarapur unit also adds dedicated quality-control, microbiology, warehousing, solvent-recovery and effluent-treatment infrastructure.
The next disclosed item to watch is F-10’s integration into Anuh Pharma’s group-wide quality-management system following its 20 October 2026 inauguration. The presentation identifies the facility’s installed capacity and technical infrastructure, but leaves commercial utilisation, product allocation and ramp-up timing unresolved.